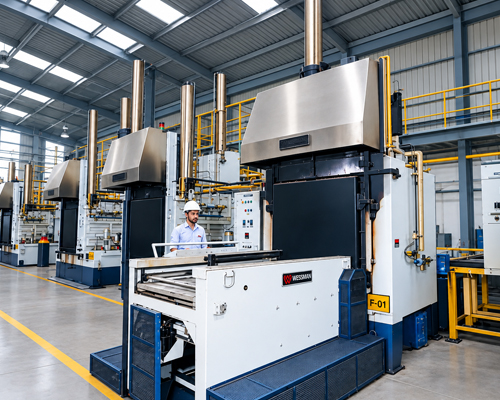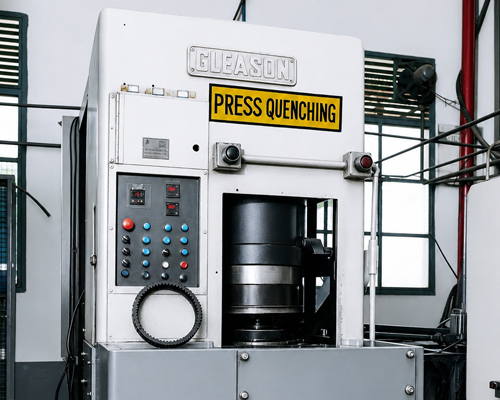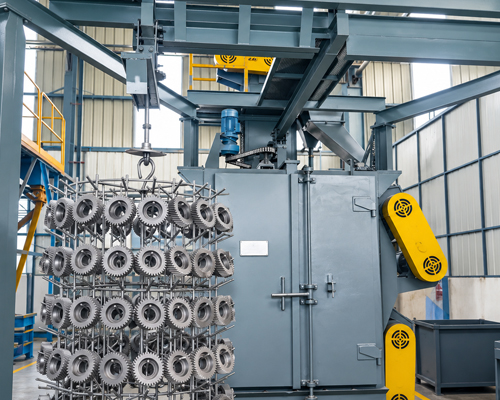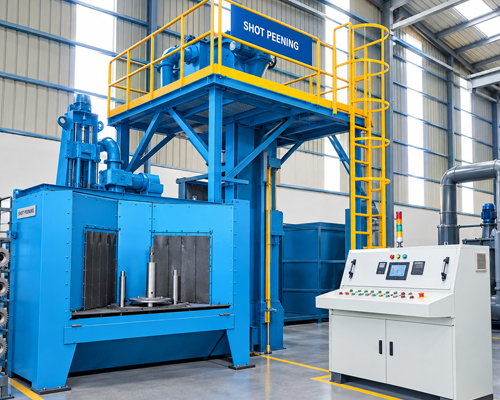
Our SCADA-monitored, CQI-9 compliant facilities run seven core processes —
normalising, isothermal annealing, controlled cooling, hardening and tempering,
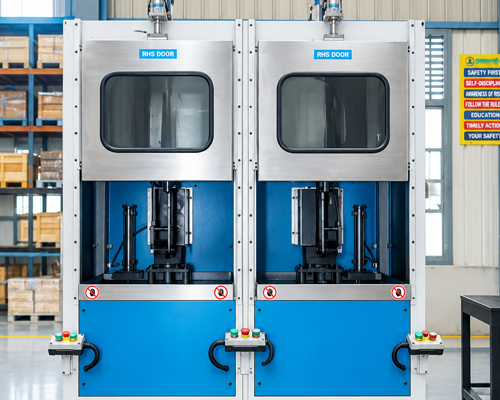
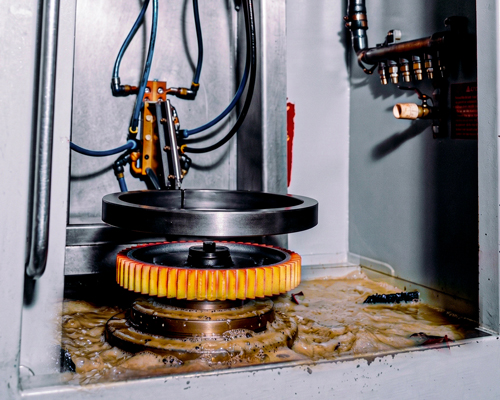
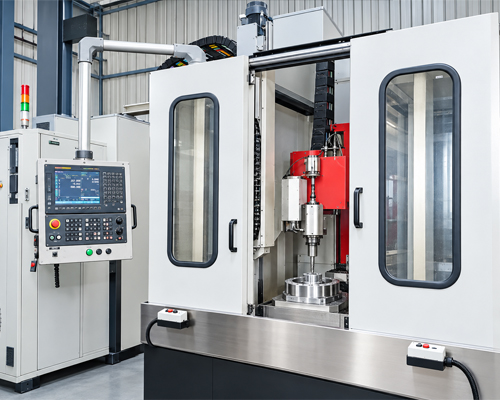
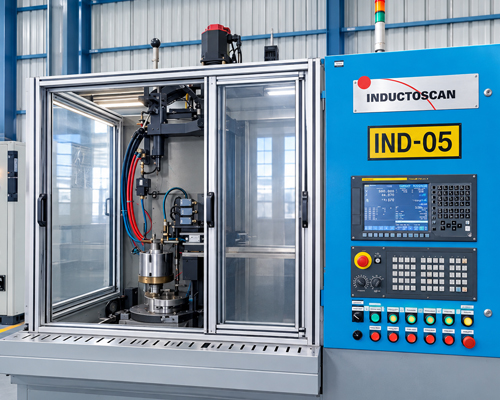
atmosphere-controlled gas carburising, press quenching, and induction hardening
and tempering — giving complete command over case depth, core hardness and
distortion for every component we make.
The line is anchored by sealed-quench furnaces with 1,500 kg charge capacity for
carburising under precisely controlled atmospheres, and induction hardening
systems from 50 kW to 600 kW covering everything from selective hardening of
small levers to deep-case treatment of heavy shafts and gears.
Every cycle is recipe-driven and digitally logged, so each batch carries a verifiable
thermal history — and every part leaves with the metallurgy its application
demands.