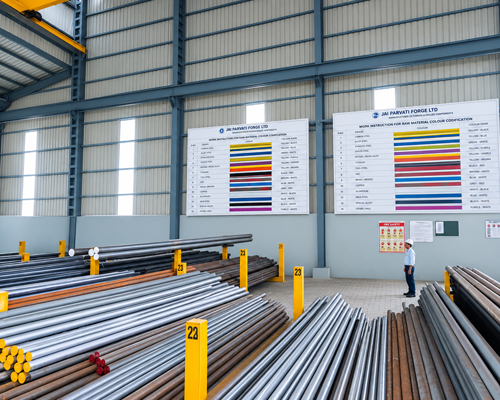
Raw material storage yard
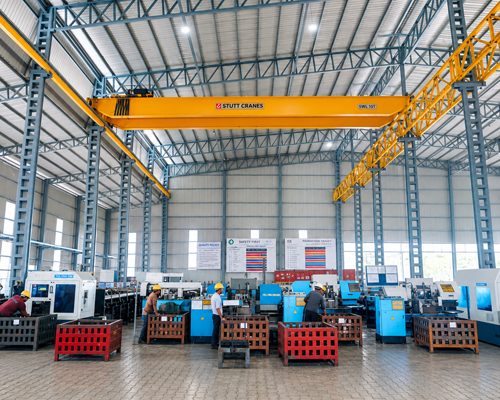
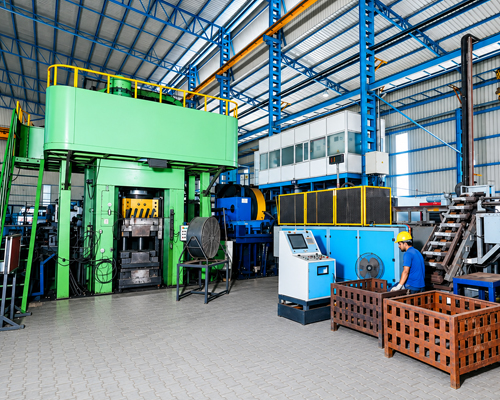
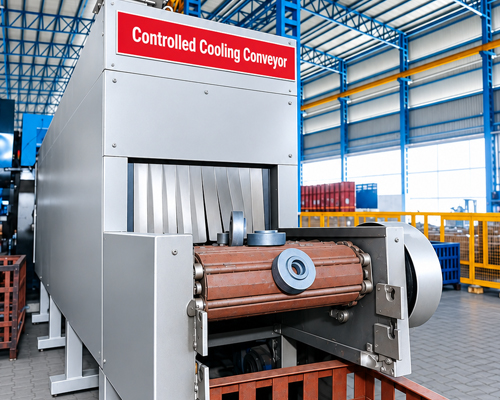
Automated hammer and press lines with induction billet heating, controlled cooling and shot blasting — roughly 32,100 MT per annum today.
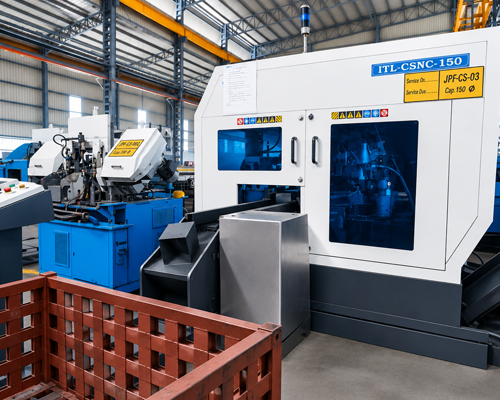
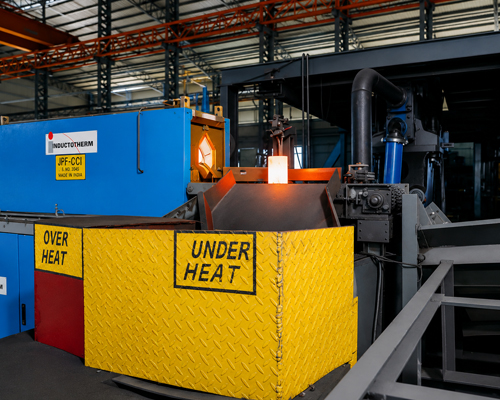
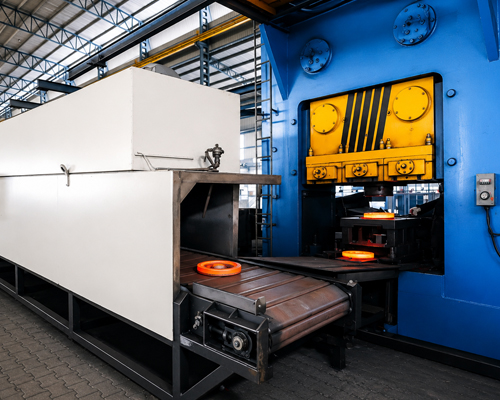
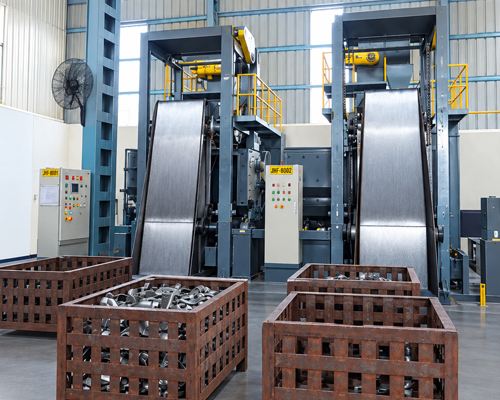
CNC billet sawing and induction billet heating with three-way temperature sorting — no under- or over-heated billet reaches the die.
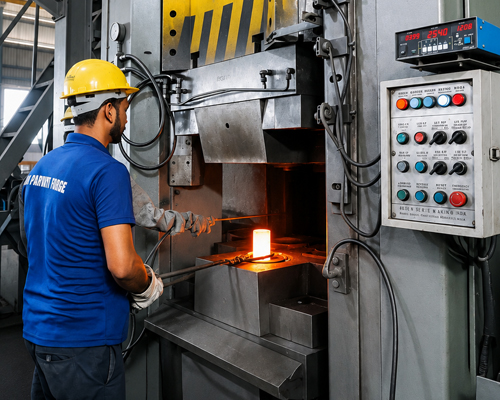
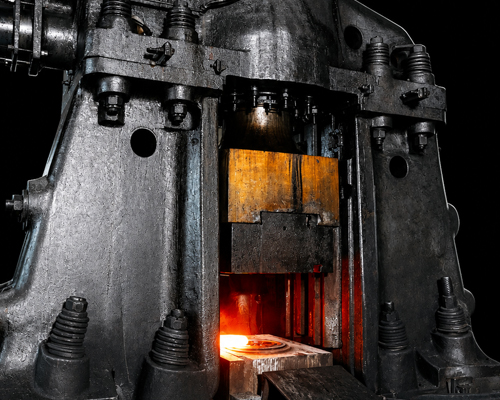
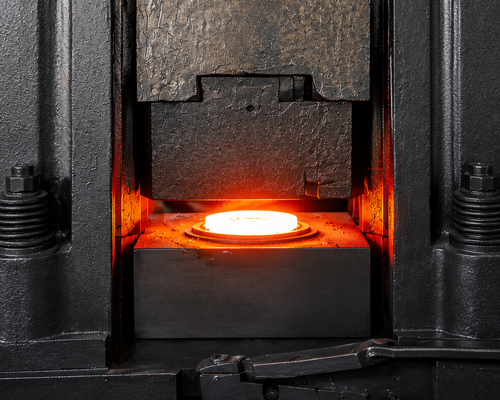
Air-operated MPM hammers, belt-drop hammers and screw presses cover 1–70 kg; heavy shafts and bull gears on the 6.25-ton hammers.
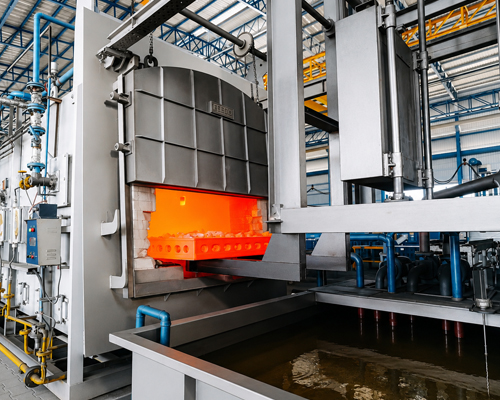
Batch-type continuous furnaces for normalising, isothermal annealing, hardening & tempering, spheroidal annealing and controlled cooling
Shot blasting, trimming and 100% visual inspection before forgings move to machining.